Search News
Industry Portal
Hot Articles
- How to assess a chlorination system OEM supplier's dosing accuracyAssess a chlorination system OEM supplier with confidence. Discover how to verify dosing accuracy, test conditions and control performance before you buy.
- Jordan to Highlight Water Investment Opportunities at EU ConferenceExplore Jordan water investment opportunities at the 2026 Jordan–EU Investment Conference, from desalination and wastewater treatment to energy efficiency.
- How to check sludge resource recovery compliance before land applicationSludge Resource Recovery compliance starts before land application. Learn how to verify test results, treatment records, and field-specific requirements.
Popular Tags
Industry NewsCan SCADA Be Integrated into an Existing Wastewater Plant?
auth.
Dr. Victor GearTime
Oct 20, 2026Click Count
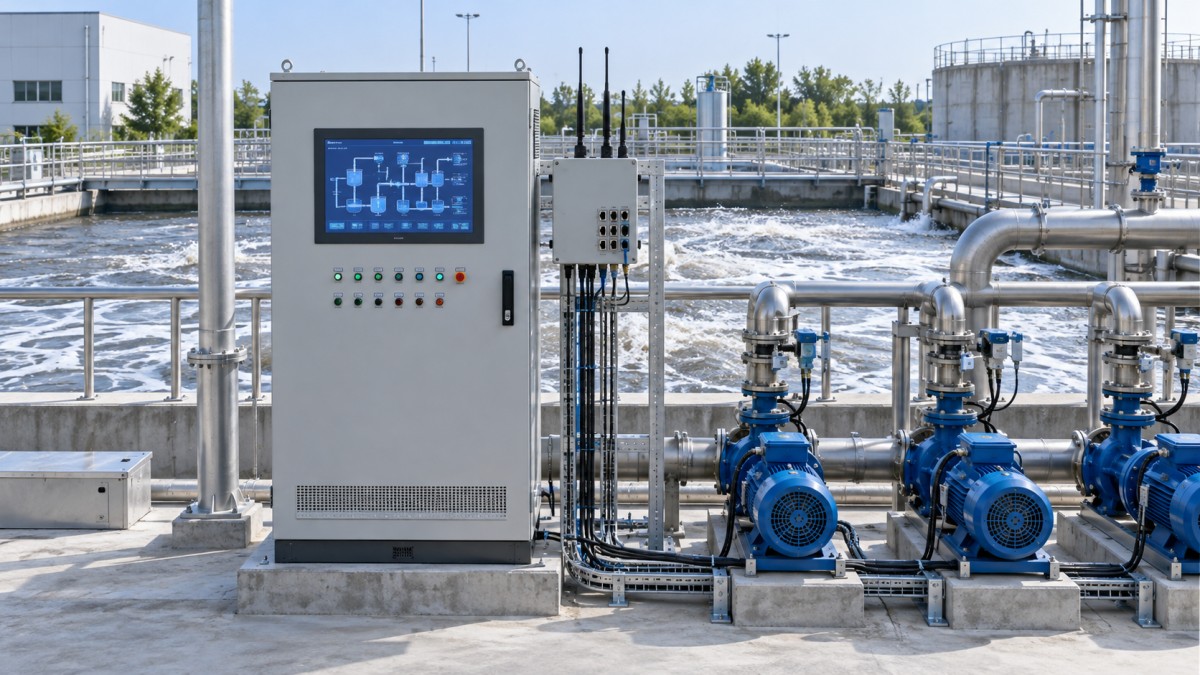
Can SCADA integrate with an existing wastewater plant? Yes—often without replacing every controller or field instrument. A supervisory control and data acquisition retrofit can connect compatible equipment, consolidate operating information, and introduce remote supervision while retaining local process control. Feasibility depends on controller access, communication interfaces, instrument reliability, and whether changes can be introduced without interrupting treatment.
The practical challenge appears when a plant has separate screens for pumping, aeration, and sludge handling, while operators still record some readings manually. Connecting those systems can improve visibility, but an incorrect tag mapping, conflicting command, or network failure could disrupt equipment operation. The safest starting point is therefore a compatibility assessment followed by a read-only pilot—not an immediate transfer of all control functions.
Decide what the retrofit must actually change
“Integrating SCADA” can mean adding a central monitoring screen, replacing an unsupported supervisory system, or enabling coordinated control across process areas. These are different projects. Define the operational problem before specifying servers, software licenses, or network hardware.
For example, unexplained blower energy use requires reliable power measurements alongside airflow, dissolved oxygen, and operating-state data. A screen showing only whether a blower is running will not explain the energy demand. Likewise, repeated wet-well high-level alarms may require better event records and alarm handling rather than a new control algorithm.
Separate requirements into monitoring, supervisory commands, reporting, and future optimization. This helps prevent a limited visibility upgrade from becoming an uncontrolled automation replacement. It also establishes which assets need two-way communication and which can remain read-only.
Keep essential control local. Pump sequencing, equipment protection, and other functions needed to maintain safe operation should remain in suitable local controllers or hardwired circuits. SCADA may issue authorized setpoints and commands, but loss of the supervisory server should not disable essential treatment functions.
Check compatibility at the controller, signal, and network levels
A controller with an Ethernet port is not automatically ready for integration. Its protocol, firmware, available connections, software access, and processing capacity all matter. Begin with an asset register that records controller models, program backups, communication modules, network addresses, instrument signals, and support status.
Common interfaces include Modbus RTU, Modbus TCP, OPC UA, and manufacturer-specific protocols. A gateway can bridge some communication differences, but it does not repair missing documentation or unreliable control logic. Legacy protocols may also lack authentication and encryption, requiring protection through network design rather than protocol settings alone.
Verify representative tags against physical equipment. A pump status may indicate a command, a contactor state, or confirmed operation; those are not interchangeable. Analog values need units, scaling, valid ranges, and quality indicators. Check whether timestamps originate in the device or supervisory system and whether totalizers survive a restart.
Instrument condition is equally important. A drifting dissolved oxygen probe or unreliable level transmitter will produce misleading trends regardless of the SCADA software. Calibration, cleaning access, and maintenance responsibilities belong in the integration scope.
Connect systems without creating competing control paths
A typical retrofit connects field instruments to PLCs or remote terminal units, then carries approved process data over an operational technology network to SCADA servers, operator workstations, and a historian. Older serial devices may sit behind gateways. Business reporting systems should receive data through controlled interfaces rather than unrestricted access to controllers.

Draw the proposed architecture before procurement. Identify network zones, permitted communication paths, server dependencies, remote-access entry points, and the boundary between monitoring and control. A flat network connecting office computers, vendor laptops, and process controllers increases the chance that an incident outside the treatment process affects operations.
When old and new supervisory systems run together, define command ownership explicitly. Read-only access from the new system is usually easier to validate. Once commands are enabled, mode selection and arbitration must prevent both systems from changing the same setpoint or issuing conflicting start and stop instructions.
Consider communications failure as an operating condition, not merely an IT fault. Screens should clearly distinguish a current measurement from a stale value. Local controllers need defined responses to lost supervisory communication, and operators need an understood fallback for essential equipment.
Redundancy should follow the operational consequence of failure. Redundant servers do not eliminate a single vulnerable network switch or power supply. Conversely, a monitoring-only installation may not justify the same architecture as a plant that depends heavily on centralized supervision.
Use a staged commissioning sequence
A retrofit can often proceed while treatment continues, but that does not mean every modification is interruption-free. Controller downloads, panel wiring, firmware changes, and network cutovers may require planned isolation or a temporary operating arrangement. Schedule these activities around process capacity and available standby equipment.
- Capture the baseline. Back up controller programs, supervisory configurations, and network settings. Document current operating modes, interlocks, alarm behavior, and unresolved faults. Confirm that backups can actually be restored.
- Build and test away from the live process. Validate drivers, tag databases, screen navigation, user permissions, and command handling using suitable simulation or test equipment. Write acceptance criteria before testing begins.
- Run a representative read-only pilot. Select a bounded area with manageable consequences. Compare displayed values against local indications and existing records, then observe communications loading and data quality under normal operation.
- Introduce alarms and historical records. Confirm timestamps, alarm priorities, event capture, and reporting calculations before operators rely on the new system.
- Enable supervisory control selectively. Test local/remote selection, command acknowledgement, permitted setpoint ranges, and interlocks. Commission one process area at a time with an agreed rollback procedure.
- Complete operational handover. Deliver current drawings, backups, licenses, maintenance instructions, and training. Assign responsibility for changes after acceptance.
Rollback criteria should be specific. Unexpected controller loading, unreliable status feedback, or unexplained equipment behavior should trigger suspension of the affected integration step. Restoring the previous configuration must be practical within the available operating window.
Make alarms and trends usable during an upset
Importing every available controller alarm can overwhelm operators. Review alarms according to the consequence of the condition and the response required. Equipment status changes may belong in an event log rather than an audible alarm list.
For each actionable alarm, define its trigger, priority, delay, deadband, operator response, and reset behavior. Communication failures need clear indication, but should not automatically create an unmanageable flood of secondary alarms. Any suppression logic must be documented so it does not hide a real process problem.
Historical data should support specific operating questions. To investigate aeration performance, align dissolved oxygen, airflow, blower power, basin status, and relevant loading information. For pumping problems, correlate level, pump commands, confirmed running states, and flow. Recording intervals should reflect process dynamics and available storage, not a uniform setting applied to every tag.
Energy comparisons need context. Track consumption against an appropriate operating measure, such as treated volume, and retain relevant process conditions. Apparent savings caused by lower flow or reduced treatment duty are not evidence that the retrofit improved efficiency. Automated compliance reports likewise require validation against applicable reporting requirements and underlying measurements.
Protect the retrofit and plan its ongoing cost
Cybersecurity should be part of the design before remote access is enabled. Separate operational systems from general business networks, permit only necessary traffic, and apply role-based permissions. Remote support should use a controlled access path with strong authentication, logging, and the ability to revoke access promptly.
Existing controllers may not tolerate the same scanning or update practices used for office computers. Assess patches and security tools for operational compatibility, test disruptive changes offline where possible, and use scheduled maintenance windows. Maintain recoverable backups of PLC logic, SCADA configuration, historian settings, and critical network devices.
A SCADA alarm is not a substitute for an independent protection function. Where equipment protection or safety depends on a dedicated interlock, integration must preserve that function and its required independence. Any change to control authority needs review by personnel responsible for process operation, electrical systems, and automation.
The project budget should include more than software and screens:
- Controller interfaces, gateways, remote I/O, and necessary instrumentation repairs.
- Network improvements, industrial hardware, power protection, and any justified redundancy.
- Engineering, tag verification, alarm configuration, commissioning, and temporary operating arrangements.
- Licenses, support, cybersecurity maintenance, backup testing, training, and future migration.
Request clear ownership and export rights for configuration files, tag databases, historical records, and custom logic. Confirm whether license limits apply to tags, clients, drivers, or redundancy. A low initial price can conceal recurring costs or make later modifications dependent on a single supplier.
Set acceptance criteria before authorizing full rollout
Acceptance should demonstrate reliable operation, not simply successful screen loading. Test loss of communication, server restart, restoration from backup, stale-data indication, user permissions, and recovery of historical recording. Exercise command paths under controlled conditions and confirm that essential local control continues when SCADA is unavailable.
Operators should also verify that displayed equipment states match reality, alarms identify a clear response, and manual operation remains accessible where required. Record unresolved limitations rather than treating them as undocumented assumptions.
Proceed when the plant has verified interfaces, trustworthy signals, clear control ownership, and a tested migration path. Narrow the initial scope when documentation is incomplete or operational redundancy is limited. Where unsupported controllers or inaccessible programs make integration unreliable, targeted replacement may be safer than adding successive gateways. That distinction determines whether SCADA becomes a maintainable operational tool or another layer of uncertainty.
Recommended News
TIME
{item.publish_time}{item.title}{item.description}auth.
{item.goods_category_sif3qfva9d}Read MoreCONTACT US